
05
Oct
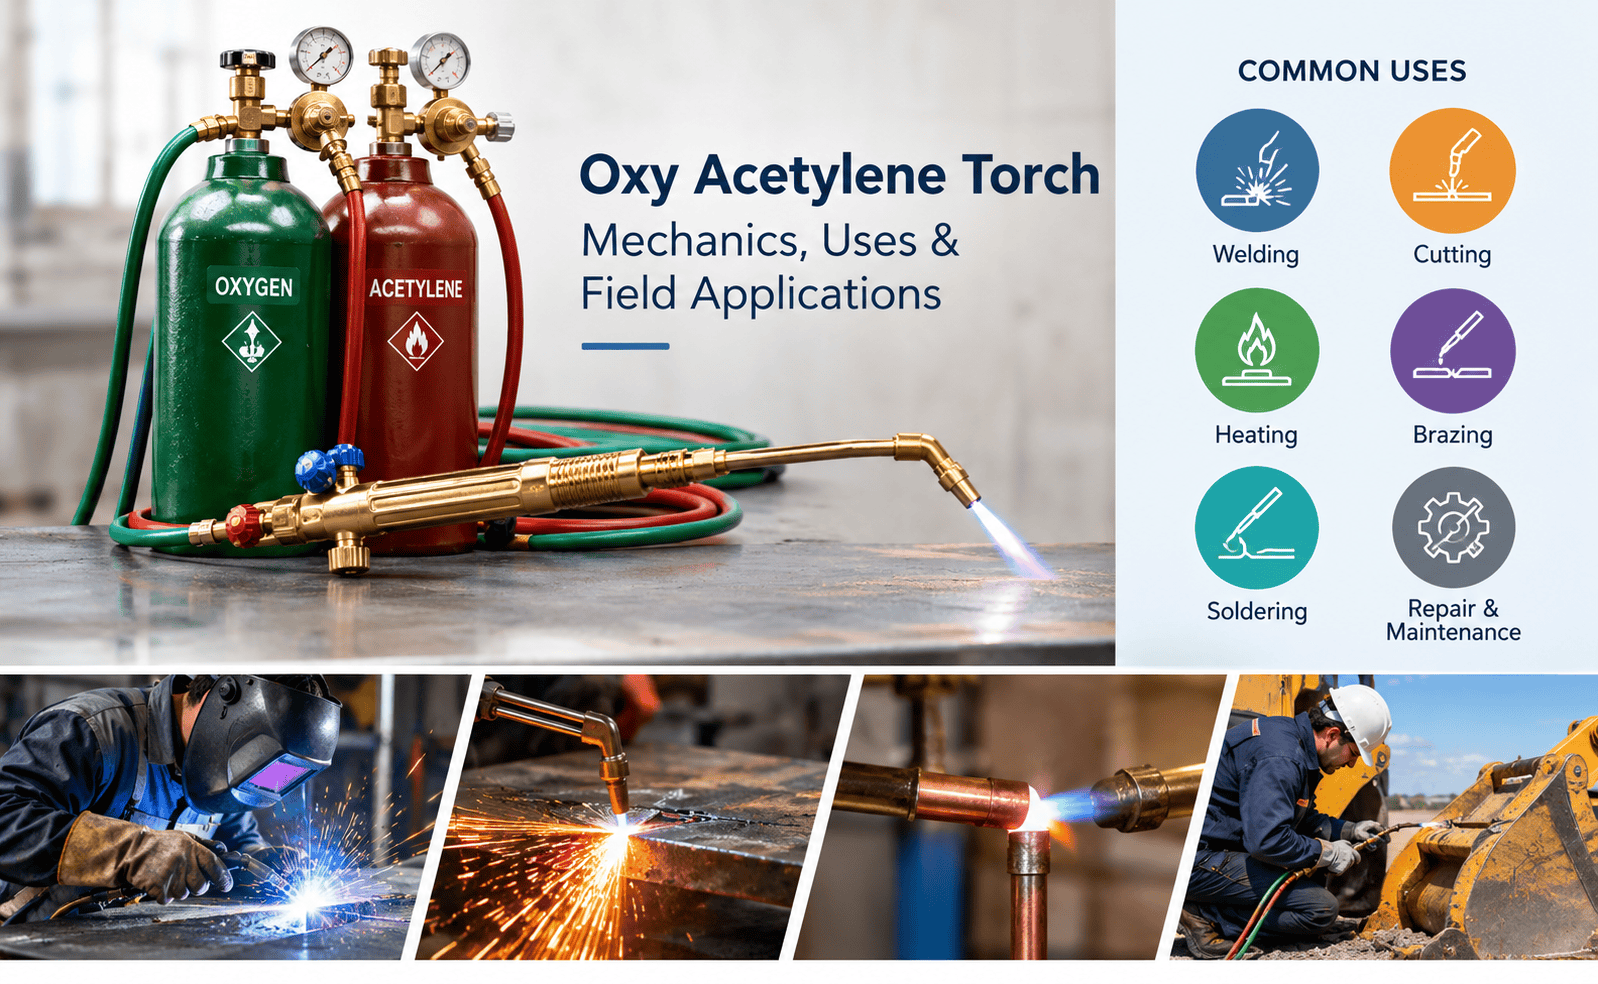
An oxy acetylene torch is a dual-gas apparatus that mixes pure oxygen with acetylene fuel gas to produce a concentrated, ultra-high-temperature flame. Heavy industrial sectors rely on this tool for fusion welding, thermal slicing, plate preheating, brazing, and mechanical heat-straightening.
Oxy Acetylene Torch: Mechanics, Uses, and Field Applications
Modern steel fabrication runs on an array of high-tech thermal systems. Even so, basic gas rigs stay anchored in the beds of mobile repair trucks and on shop floors across Ontario. Electric arc gear is everywhere, but an oxy acetylene torch gives you an intense heat source without plugging into a generator or hunting for an electrical drop.
Steel reacts predictably to direct chemical heat. When you stand in a muddy staging yard, out on an exposed beam, or inside an active processing plant across Toronto, holding that concentrated flame gives you immediate leverage over stubborn iron. Fabricators reach for it daily because it handles awkward physical tasks that electric tools simply cannot touch.
Fundamentals of the Oxy Acetylene Torch System
The entire setup hinges on the combustion chemistry between pressurized fuel gas and high-purity industrial oxygen. Acetylene stands apart from other fuel gases like propane or propylene. Its triple-bonded carbon structure releases massive amounts of thermal energy the instant it cracks open in an oxygen stream. That reaction easily melts structural carbon steel.
The physical rig includes separate high-pressure cylinders, two-stage brass regulators, color-coded supply hoses, internal check valves, inline flashback arrestors, and the torch handle itself, which accepts modular mixer blocks and copper tips.
Everything starts at the bottle valves.
Acetylene cylinders contain a porous silicate mass soaked in liquid acetone, which stabilizes the dissolved gas under pressure. Cracking the fuel valve feeds vapor into a regulator calibrated strictly for low operating pressures. Oxygen tanks hold dry gas at roughly 2,200 pounds per square inch. That massive pressure requires immaculate valve seats and a complete absence of oil, grease, or pipe dope.
The gases flow through separate rubber lines to reach the mixer block in the handle. There, machined channels blend them in exact ratios before the mixture shoots through the nozzle orifice. Precision drilling inside those copper tips governs flame velocity, spread, and overall stability.
Flame Chemistry and Operational Dynamics
Running clean cuts or sound welds requires reading the flame at the copper nozzle tip. The operator cracks the fuel valve first, striking a smoky yellow plume that sheds loose flakes of soot. Cracking the oxygen knob draws that yellow curtain down into a sharp, luminous inner cone. How you balance that mix sets your working heat transfer rate and keeps the molten puddle clean.
Differentiating Neutral, Carburizing, and Oxidizing Flames
A neutral flame forms when the volumetric ratio between oxygen and acetylene reaches balance. You can spot it by its smooth, bright white inner cone with no feathered tail around the perimeter. It neither pumps excess carbon into the joint nor burns away the iron. That clean profile makes the neutral flame the baseline standard for fusion welding, localized preheating, and braze-welding carbon steels.
Open the fuel knob further, and a soft white brush known as an acetylene feather spills past the cone tip. This carburizing or reducing flame injects unburnt carbon straight into the metal puddle. Welders use this trait deliberately when working high-carbon tool steels or setting up hard facing overlays where surface carbon loss would wreck wear resistance.
Turn the oxygen up too high, on the other hand, and you get an oxidizing flame. The inner cone shrinks, points sharply, and emits a harsh hiss. That flame burns hotter, but it aggressively rots raw steel into spongy slag unless you are purposefully running specialized brass brazing runs.
Primary Oxy Acetylene Torch Uses in Fabrication and Repair
Versatility keeps this tool in daily service. While automated CNC tables or high-amp plasma units handle repetitive cuts, an experienced tradesperson changes a copper tip, tweaks two regulator knobs, and moves an oxy acetylene torch from delicate sheet-metal silver brazing to chewing through six-inch crane counterweights. That physical flexibility makes the rig invaluable for field mechanics roaming industrial corridors across the Greater Toronto Area.
Oxy Acetylene Welding Compared to Thermal Cutting
The mechanical difference between gas welding and gas cutting is fundamental. In oxy acetylene welding, the operator plays a neutral flame across base metal edges until they liquefy into a shared puddle. Dipping a bare filler wire by hand builds the joint cross-section, which cools into a permanent structural seam. Atmospheric shielding comes entirely from the combustion gases surrounding the weld zone.
Cutting metal relies on a completely different phenomenon: rapid chemical oxidation. The cutting head houses several small preheat orifices clustered around an independent central port. Those outer preheat flames bring the target steel up to its kindling threshold (around 1,600 degrees Fahrenheit), marked by a distinct cherry-red glow.
Also read: 10 Plasma Cutter Types (& How to Choose the Right One for Your Project)
Once that color appears, the operator squeezes the high-pressure cutting lever. A blast of pure oxygen strikes the red-hot steel, burning the iron into molten iron oxide. The velocity of the gas blows that slag out the underside of the plate. You are not melting the gap; you are burning it away under pressure.
Metal Straightening, Preheating, and Seized Part Removal
Intense heat does far more than just cut and fuse. Heavy structural members often pull out of shape after high-heat multi-pass arc welding. Fabricators correct those bends using multi-flame heating heads, known across the trade as rosebuds, to work line heat or wedge heat into the deformed flange. The heated zone wants to expand, but cold surrounding steel blocks it, forcing the hot spot to upset and thicken. As that area cools back to ambient temperature, it shrinks tight, pulling heavy beams back into plumb.
Millwrights also lean on the rosebud to free heavy industrial gear locked solid by rust. When hydraulic pullers stall on frozen bearing sleeves, seized crane pins, or corroded pipe flanges, direct heat breaks the bond. Warming the outside collar causes it to expand rapidly before the inner shaft absorbs the heat, which frees the trapped components without scoring precision surfaces.
Oxy Fuel Cutting Versus Alternative Severing Methods
Selecting the best cutting method depends on stock thickness, job location, electrical supply, and post-cut cleanup needs. Fabricators routinely weigh oxy fuel against plasma arc setups and mechanical bandsaws.
Plasma setups cut non-ferrous metals like aluminum, stainless steel, and bronze with ease. Standard oxy fuel equipment cannot cut those metals because their oxides form a protective crust rather than burning freely. Plasma also cuts light sheet metal faster with less heat warp. Cold saws leave smooth, square cuts ready for fit-up without edge grinding.
Yet the oxy acetylene cutting torch dominates when you face thick carbon steel plate, heavily rusted structural members, or layered scrap metal. Plasma units choke on thick rust scale and require heavy three-phase power lines alongside high-volume shop air. Out in an open field, on a bridge demolition, or beside a stranded highway excavator, a mobile gas rig works alone. It cuts clean through heavy iron where electric tools stop dead.
Essential Protocols for Oxy Acetylene Torch Safety
Handling compressed fuel and high-pressure oxidizers demands relentless attention to detail. Concentrated fuel, high oxygen levels, radiant heat, and white-hot slag create major fire hazards if valves fail or workers take shortcuts.
Flashbacks are the most dangerous hazard on the job. A flashback happens when the flame burns back through the mixing chamber and runs upstream into the rubber hoses. It creates a sharp popping or shrill squeal, accompanied by foul smoke and rapid handle heating.
When this occurs, shut the oxygen valve instantly, then kill the fuel valve. To stop fire from reaching the tanks, every commercial rig needs certified flashback arrestors mounted at the torch handle inlets and regulator outlets, backed by functional reverse-flow check valves.
- Inspect rubber hoses for dry rot, deep scuffs, blisters, and grease spots before turning any tank valves.
- Check that heavy steel securing chains hold every bottle upright and stable against a wall or cart.
- Purge each supply hose individually for several seconds prior to lighting up to clear blended air pockets.
- Light the tip with an approved friction spark striker; never use disposable butane lighters or matches.
- Keep working fuel pressures inside safe equipment specs, never running free acetylene gas above 15 psi.
- Put on shaded cutting goggles, split-leather gauntlets, and heavy cotton or leather work gear.
- Sweep away sawdust, cardboard boxes, solvent cans, and fuel containers from the drop zone beneath your cut.
- Set a charged ABC dry chemical fire extinguisher within arm’s reach before starting your preheat.
Mobile Welding and On-Site Field Work Across the GTA
Commercial operations throughout southern Ontario deal with sudden structural cracks that threaten hard job deadlines. Hauling broken earthmoving buckets, bent trailer chassis, or damaged building lintels back to a fixed shop burns hours you cannot spare. Professional RS mobile welding crews, resolve those jams by bringing fully outfitted service rigs straight to construction jobs, transit lines, and transfer depots across Toronto.
Field mechanics rely on portable gas rigs to handle emergency on-site welding GTA demands. They wash out cracked fillet welds on backhoes, trim misaligned columns on commercial job sites, and free rusted industrial drive shafts. Carrying self-contained thermal cutting and heating equipment eliminates project delays.
When sudden repairs stop work on your site, dispatching certified mobile welders ensures every cut, gouge, and structural joint meets strict safety codes while keeping workers and assets secure.
Frequently Asked Questions
What is an oxy acetylene torch used for?
An oxy acetylene torch is primarily used for thermal cutting of carbon steel, fusion gas welding, localized heating for metal straightening, flame gouging, brazing dissimilar metals, and expanding seized industrial hardware during mechanical maintenance.
Can an oxy acetylene torch cut steel of any thickness?
The system severs carbon steel ranging from light structural tubing up to extremely thick industrial slabs, provided the operator matches the cutting tip orifice diameter and gas supply volume to the specific cross-section of the workpiece.
What is the difference between oxy acetylene welding and cutting?
Welding uses a balanced flame to melt joint edges together alongside a filler rod, creating a solid structural bond. Cutting uses the outer flame strictly to preheat the steel, followed by an independent blast of pure oxygen that chemically oxidizes and clears the iron away.
Why is oxy acetylene cutting safe only when proper procedures are followed?
The process involves highly pressurized gases, intense thermal radiation, and rapid chemical reactions that can cause severe explosions, flashbacks, or structural fires if equipment lacks proper arrestors, maintenance, ventilation, and operator training.

RS Welding
" Raj and Khushmeet lead RS Mobile Welding Service with 25+ years of experience delivering expert welding and fabrication across Toronto and the GTA. Backed by Canadian Welding Bureau certification, their team handles everything from emergency repairs to custom metal work with precision, safety, and reliability. When you need mobile welding done right, RS gets it done right."